International Fluid Power Inc.
International Fluid Power - Innovative Partners For Global Sourcing Of Fluid Power Products. Your Complete Hydraulic Source in SE Minnesota.
Choosing the China Best Blind Flanges Manufacturer and Supplier requires more than comparing prices. It requires evidence.
The global industrial valves market continues to expand, according to Grand View Research. Its industry report identifies infrastructure investment, energy projects, and process manufacturing as major growth drivers. These sectors also create steady demand for reliable Blind Flanges. However, market growth does not guarantee supplier quality.
A serious manufacturer should demonstrate material traceability, dimensional control, and pressure-testing records. Look for certificates covering ASTM, ASME, EN, or equivalent requirements. Request heat numbers, inspection reports, and clear tolerances. A flange may appear perfect on a warehouse shelf. Its performance depends on machining accuracy, steel chemistry, gasket contact, and installation torque.
John H. Bickford, a recognized authority on bolted-joint engineering, wrote, “The purpose of a bolt is to produce and maintain clamping force.” That principle matters here. Poor bolt loading can undermine an excellent flange.
Small details matter.
A dependable Chinese supplier should explain forging routes, ultrasonic testing, coating options, and export packaging. Wooden crates, sealed flange faces, and visible identification labels are practical signs of control. Site audits and independent inspections add confidence.
Yet no supplier is automatically perfect. Some websites show impressive certificates but provide weak technical responses. That deserves scrutiny. A careful buyer should compare production capacity, inspection depth, delivery history, and after-sales communication.
This guide examines leading China Blind Flanges manufacturers and suppliers through those practical standards. The goal is not the cheapest quotation. It is a traceable, correctly engineered product that performs when the pipeline is finally pressurized.
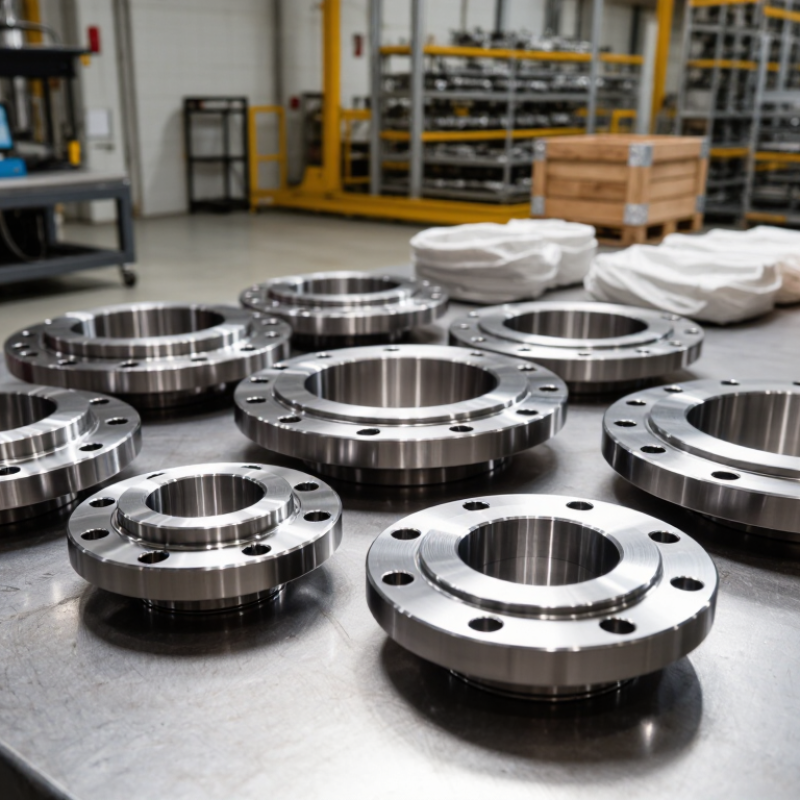
A blind flange is a solid, flat-ended flange used to close a pipe, nozzle, or vessel opening. Unlike a weld neck or slip-on flange, it has no bore. Its raised face compresses a gasket against the matching flange, while bolts create the sealing force.
Blind flanges are common at pipeline ends, pump outlets, pressure vessels, and inspection points. Operators use them during hydrostatic testing, maintenance, or future line extensions. They can isolate equipment without removing long pipe sections. The metal disc looks simple, but pressure rating, material grade, and facing details must match the system. A small mismatch can cause leakage.
In field inspections, technicians check the flange face for scratches, rust, and uneven wear. They also confirm bolt length, gasket type, and tightening sequence. The wrong gasket may fail even when the flange is correctly machined. This detail is sometimes overlooked. For high-pressure service, dimensional standards, heat treatment records, and test reports should be reviewed before shipment. A reliable Chinese manufacturer or supplier should provide traceable material certificates and clear inspection data. However, paperwork alone is not enough; random dimensional checks and visual inspection still matter. The flange may pass a factory check and fail after poor installation.
A blind flange is a solid flange without a bore. It is used to close the end of a piping system, pressure vessel nozzle, valve, or unused branch, while allowing future access for inspection or maintenance.
The chart shows the nominal outside diameter for commonly used ASME B16.5 Class 150 blind flange sizes. Actual selection must also consider pressure class, temperature, material, gasket type, bolting, and applicable project standards.
Selecting a blind flange requires more than checking its diameter.
The governing standard must match the connected piping system, pressure rating, and installation region. ASME B16.5 commonly covers flanges up to NPS 24, while ASME B16.47 applies to larger sizes. EN 1092-1 is widely used for European installations. ISO 7005 may also appear in international specifications. These standards define dimensions, bolt holes, facing types, and pressure classes.
Material selection depends on temperature, fluid, corrosion risk, and design pressure.
ASTM A105 carbon steel suits many ordinary process lines. ASTM A350 LF2 is often chosen for low-temperature service. Stainless steel forgings, such as ASTM A182 F304 or F316, provide better corrosion resistance. Duplex grades can handle demanding chloride environments, but welding and inspection require stricter control. The flange material should remain compatible with the pipe, gasket, bolts, and operating conditions.
In practical inspections, I check the marking, heat number, face finish, and bolt-hole alignment.
Small errors matter. A flange may meet a dimensional standard but still fail the project specification. I have seen drawings list a pressure class without stating the temperature basis. That detail needs review. Engineers should confirm wall thickness, corrosion allowance, gasket seating, and test requirements before ordering. A capable manufacturer should provide material certificates, dimensional reports, and traceable inspection records. Even then, paperwork is not enough; random verification remains wise.
Choosing a China blind flange manufacturer requires more than comparing prices. Begin with technical evidence. Ask for material certificates, heat numbers, dimensional reports, and pressure-test records. A reliable supplier should explain the flange standard, pressure class, facing type, and material grade without hesitation. Check whether measurements cover bolt-hole spacing, outer diameter, thickness, and sealing-face finish.
Request a sample before approving a production order. Inspect the raised face under clean light. Look for machining marks, rust stains, uneven drilling, or damaged edges. The gasket surface should match your application, not merely appear polished. Confirm how the supplier controls raw materials, heat treatment, machining, marking, and final inspection. Photos help, but an independent inspection gives stronger evidence. A polished brochure is not proof.
Communication reveals practical experience. Ask how rejected parts are isolated and how nonconforming dimensions are corrected. Check packaging details, including edge protection, moisture barriers, wooden cases, and identification labels. Export documents should match the physical goods. Small mismatches can delay installation. It is also useful to review previous project references, though references may not show difficult failures. That limitation deserves attention. A factory visit, live video inspection, or third-party audit can expose gaps between written procedures and actual work. Do not accept vague claims such as “premium quality.” Require measurable tolerances, inspection frequency, and a clear response time for technical questions. Reliability is built through records, repeatable processes, and uncomfortable questions.
A reliable blind flange supplier provides more than competitive pricing. They understand pressure systems, piping layouts, material grades, and field installation conditions. Their engineers should confirm flange size, pressure class, facing type, drilling pattern, and applicable standards before production. Small mistakes matter. A mismatched bolt circle can delay an entire project.
Experienced suppliers use controlled forging, machining, heat treatment, and dimensional inspection. They should provide material certificates, inspection records, and traceable batch numbers. Testing may include chemical analysis, hardness checks, ultrasonic inspection, and pressure testing when required. Clear records build confidence. Photos of machined surfaces and measured dimensions can also support remote quality checks.
Communication shows practical reliability. The supplier should answer technical questions directly and identify risks before accepting an order. They need realistic lead times, protective packaging, and stable export documentation. A strong quality system helps, but paperwork alone is not enough. Buyers should review samples, audit inspection methods, and compare delivered products with approved drawings. Even careful manufacturers can make occasional errors, so a responsive correction process is essential. This is where many purchasing decisions become difficult. Low prices often hide weak traceability, inconsistent machining, or delayed communication. An honest supplier admits limitations and improves the process instead of making promises that cannot be verified.
Choosing the best China blind flange partner requires more than comparing quoted prices. Start with application details: pressure class, nominal size, facing type, material grade, and service temperature. A serious supplier should confirm these points before production. ASME B16.5 or B16.47 compliance must match the flange dimensions and pressure requirements. Ask for mill certificates, heat numbers, and EN 10204 inspection documents.
Quality systems matter. The ISO Survey 2023 recorded more than 1.2 million ISO 9001 certificates worldwide, showing how common certification has become. Yet a certificate alone proves little. Request recent inspection records, dimensional reports, and material traceability examples. For critical piping, include ultrasonic testing, chemical analysis, and pressure-related verification when required. Photos should show markings, sealing faces, and protective packaging.
Check manufacturing capacity against your actual order pattern. The World Steel Association forecast global steel demand at about 1.75 billion tonnes in 2024, highlighting the scale of the raw-material market. Still, steel availability does not guarantee stable flange quality. During factory evaluation, inspect machining equipment, calibration labels, storage conditions, and final packing. A small trial order can reveal more than a polished presentation. I have seen buyers overlook gasket-face damage because the price looked attractive. That mistake is expensive. Delivery terms, replacement procedures, and communication response times also deserve written confirmation. No partner is perfect; even a strong supplier should explain its weak points clearly.
| Evaluation Dimension | Verified Technical Requirement | Relevant Standard or Reference | Documents or Evidence to Request | Recommended Acceptance Check |
|---|---|---|---|---|
| Flange Standard | Confirm whether the blind flange is manufactured to ASME B16.5, ASME B16.47, EN 1092-1, or another specified standard. Do not mix dimensional systems without written approval. | ASME B16.5 covers pipe flanges and flanged fittings for NPS 1/2 through NPS 24. ASME B16.47 covers large-diameter flanges from NPS 26 through NPS 60. | Approved drawing, standard designation, dimensional inspection report, and product marking photographs. | The standard, nominal size, pressure class, facing, bolt-hole pattern, and material are clearly stated on the quotation and drawing. |
| Nominal Size and Pressure Class | Specify nominal pipe size and pressure class together. Typical ASME B16.5 pressure classes include 150, 300, 400, 600, 900, 1500, and 2500. | ASME B16.5 and ASME B16.47 pressure-temperature rating tables. | Pressure-temperature rating table, dimensional drawing, and application design conditions. | The selected class is suitable for the design pressure, design temperature, fluid, and applicable piping code. |
| Facing Type | Common blind flange facings include raised face, flat face, ring-type joint, and other configurations defined by the applicable standard. | ASME B16.5; ASME B16.47; EN 1092-1. | Facing detail on the drawing, surface-finish report, and gasket compatibility statement. | The facing type and gasket contact dimensions match the mating flange and piping design. |
| Carbon Steel Material | ASTM A105 is a commonly specified forged carbon steel material for piping components at ambient and higher-temperature service. ASTM A350 LF2 is commonly used where low-temperature toughness requirements apply. | ASTM A105/A105M; ASTM A350/A350M; ASME BPVC Section II material specifications where applicable. | Material Test Certificate, heat number traceability, chemical analysis, tensile test, yield strength, elongation, and impact-test results when required. | The material grade, heat number, chemical composition, mechanical properties, and delivery condition match the purchase specification. |
| Stainless Steel Material | ASTM A182 F304/F304L and F316/F316L are commonly specified forged stainless steel grades. The low-carbon L grades are often selected for improved weld-area corrosion resistance. | ASTM A182/A182M; ASME BPVC Section II material specifications where applicable. | Material Test Certificate, PMI report, heat-treatment record, and corrosion-service requirements. | The selected stainless steel grade is compatible with the process fluid, temperature, chloride exposure, and welding requirements. |
| Manufacturing Process | For forged blind flanges, the manufacturing route should include controlled forging, heat treatment, machining, inspection, and traceability. The process should be defined for the selected material grade and size. | Applicable ASTM material specification; ASME B16.5 or EN 1092-1 dimensional requirements. | Process flow chart, forging procedure, heat-treatment chart, machining inspection plan, and traceability procedure. | The supplier can trace the finished flange to the original material heat and documented production records. |
| Chemical and Mechanical Testing | Testing should verify chemical composition and mechanical properties specified by the material standard, including tensile strength, yield strength, and elongation. Impact testing is required when specified by grade or service condition. | ASTM A105/A105M, ASTM A182/A182M, ASTM A350/A350M, and the purchase specification. | Heat-wise chemical report, tensile-test report, hardness results, impact-test report when applicable, and third-party inspection report if required. | Test results are heat-specific, legible, consistent with the material grade, and linked to the product identification. |
| Non-Destructive Examination | Non-destructive testing may include visual examination, liquid penetrant testing, magnetic particle testing, ultrasonic testing, or radiographic testing, depending on the specification and service risk. | ASME B16.5; ASTM E165/E165M; ASTM E709; ASTM A388/A388M; project-specific inspection requirements. | NDE procedures, operator qualifications, examination reports, acceptance criteria, and repair records. | The required NDE method, coverage, acceptance level, and reporting format are agreed before production. |
| Dimensional Accuracy | Critical dimensions include outside diameter, bolt-circle diameter, bolt-hole diameter, number of holes, thickness, bore or hub details where applicable, and facing dimensions. | ASME B16.5, ASME B16.47, or EN 1092-1, according to the order. | Dimensional inspection report, calibrated measuring-equipment list, and approved production drawing. | All measured dimensions comply with the selected standard and the approved drawing, including bolt-hole orientation and facing details. |
| Facing Surface Finish | Raised-face and ring-type-joint sealing surfaces require controlled machining and surface-finish verification. The specified finish must be stated rather than assumed. | ASME B16.5 and the applicable project or gasket specification. | Surface-finish measurement report, machining record, and photographs of the sealing face. | The sealing surface is free from damaging scratches, dents, laps, cracks, and corrosion that could affect gasket performance. |
| Pressure Testing | Blind flanges are pressure-boundary components, but the required hydrostatic or other pressure testing should be defined by the purchase specification and applicable piping code. Testing requirements are not automatically identical for every order. | Project piping code, purchase specification, ASME B16.5 or EN requirements where applicable. | Pressure-test procedure, calibrated gauge certificates, test record, test medium, duration, and acceptance result. | The test pressure, holding time, temperature, gauge range, and acceptance criteria are approved before testing. |
| Marking and Traceability | Product identification should remain readable after manufacture and coating. Marking normally includes material grade, nominal size, pressure class, facing designation, standard, and heat or lot number as specified. | Applicable flange standard and purchase specification. | Marking layout, nameplate or product photographs, packing list, and heat-number traceability records. | The marking on the flange matches the certificate, drawing, packing list, and purchase order. |
| Quality Management | A documented quality-management system should control purchasing, production, inspection, nonconformity handling, corrective action, and record retention. | ISO 9001 quality-management-system principles. | Valid quality certificate, quality manual summary, inspection and test plan, internal audit evidence, and nonconformity procedure. | The certificate scope covers the relevant manufacturing or trading activity and can be verified with the issuing certification body. |
| Coating and Corrosion Protection | Protection may include oiling, rust preventive treatment, painting, galvanizing, or other specified coatings. Stainless steel products require handling controls to avoid contamination. | Purchase specification, project coating specification, and material-specific handling requirements. | Coating procedure, coating inspection report, dry-film thickness report when applicable, and packing photographs. | The protection method is suitable for storage, transportation, service environment, and the required final surface condition. |
| Packaging and Export Readiness | Flanges should be protected against impact, moisture, contamination, and deformation during transport. Sealing faces and machined surfaces require particular protection. | Purchase order, logistics requirements, and destination-country import requirements. | Packing specification, package photographs, packing list, country-of-origin documentation, and shipping marks. | The packing method supports safe handling, clear identification, moisture protection, and efficient receiving inspection. |
| Commercial Capability | A suitable partner should provide a clear quotation covering standard, size, class, material, facing, quantity, inspection scope, packaging, delivery terms, and validity period. | Buyer purchase specification and agreed commercial terms. | Itemized quotation, technical deviation list, manufacturing schedule, payment terms, and quality-document index. | Technical exclusions, substitutions, tolerances, inspection costs, tooling charges, and delivery responsibilities are written clearly. |
| Final Supplier Selection | Choose the partner that demonstrates consistent compliance, complete traceability, transparent documentation, reliable communication, and practical control of quality and delivery risks. | Approved vendor procedure and project-specific procurement requirements. | Completed supplier questionnaire, sample document package, reference project evidence without confidential information, and pre-production meeting record. | Select on documented technical compliance and total project risk, not on unit price alone. |
This is an example of a widget area that you can place text to describe a product or service. You can also use other WordPress widgets such as recent posts, recent comments, a tag cloud or more.
© 2025 International Fluid Power, Inc. All Right Reserved.